High Performance Rail Unloader
Product Details:
Innovative Drive Mechanism:
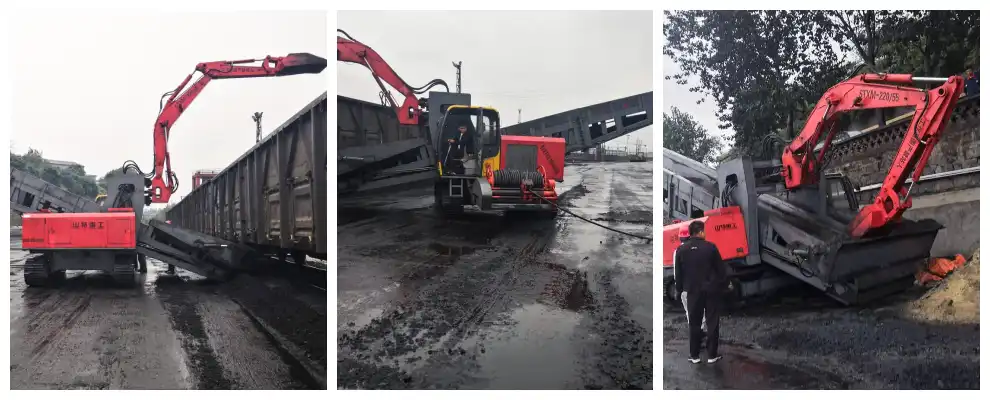
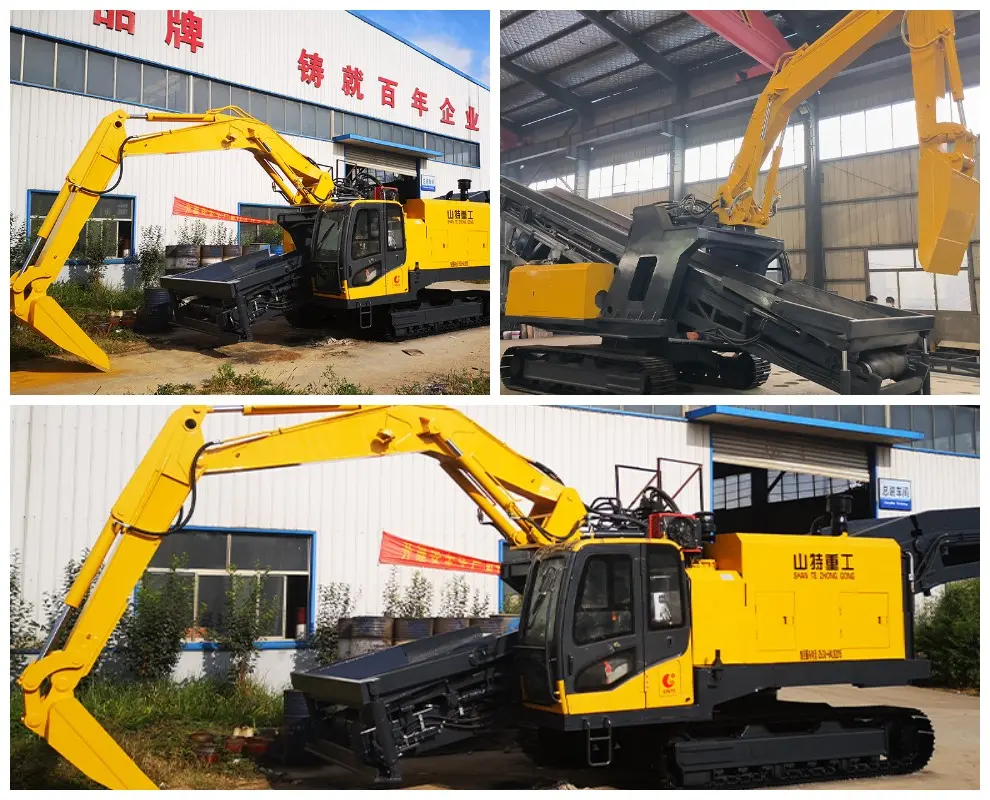
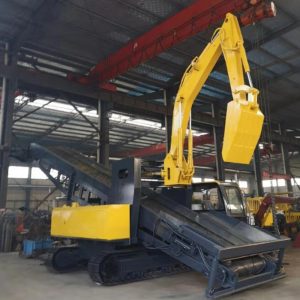
Equipped with a three-phase electric motor, the conveyor-based unloader ensures adaptable performance with minimal upkeep, emission-free operation, and reduced downtime. The electric propulsion system cuts operational expenses by 66% compared to conventional engine-driven alternatives.
Sustainable Material Handling:
Engineered to eliminate coal spillage and airborne particulate contamination. Its rear-loading design enables direct coal transfer to transport units, aligning with energy conservation and ecological regulations.
Space-Optimized Inlet Structure:
A tightly sealed feeding mechanism prevents coal deposition on rail tracks, preserving worksite hygiene and minimizing post-task cleaning labor.
Comprehensive Extraction Capability:
Guarantees complete coal evacuation from cargo compartments, alleviating manual residue removal workloads.
Climate Control Technology:
Incorporates an intelligent HVAC system delivering multidimensional airflow, continuous air renewal, and ozone-safe refrigerants for enhanced operator ergonomics.
Operational Excellence:
Synchronized dual-pump hydraulics and multi-function automation elevate material transfer rates and process efficiency.
Company Profile:
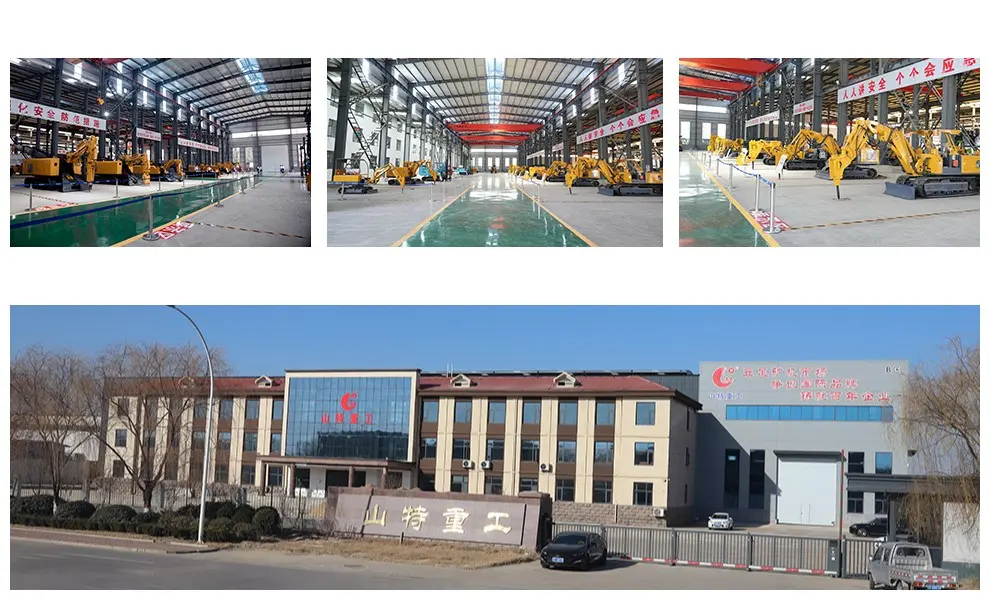
As a key player since 2009, Shandong Shante Heavy Industry specializes in heavy machinery for mining and water conservancy. Its 10-hectare complex manufactures 20+ models, including electric excavators and hydraulic milling machines, serving coal mines, railways, and ports across China and 30+ countries. The company’s accolades span National High-Tech Status, Provincial Integrity Awards, and safety certifications from the Anbiao Center. Through partnerships with Shandong University’s Innovation Base and a municipal technology lab, Shante advances R&D while producing 3,000 units annually, cementing its role as an industry trailblazer.
 Shandong Famousbrain Heavy Industry Machinery Co., Ltd.
HelloPlease log in